One-Cavity Crate Production Line: Setup, Cycle Time and Cost (2026)
Direct answer: A one-cavity crate production line molds one plastic crate per cycle on a 650–1,000 t machine with a single-cavity hot-runner mold. It fits 400×300 mm to 600×400 mm turnover boxes
Direct answer: A one-cavity crate production line molds one plastic crate per cycle on a 650–1,000 t machine with a single-cavity hot-runner mold. It fits 400×300 mm to 600×400 mm turnover boxes, runs 18–35 s cycles and produces 180 crates an hour gross at a 20 s cycle.
What the line includes
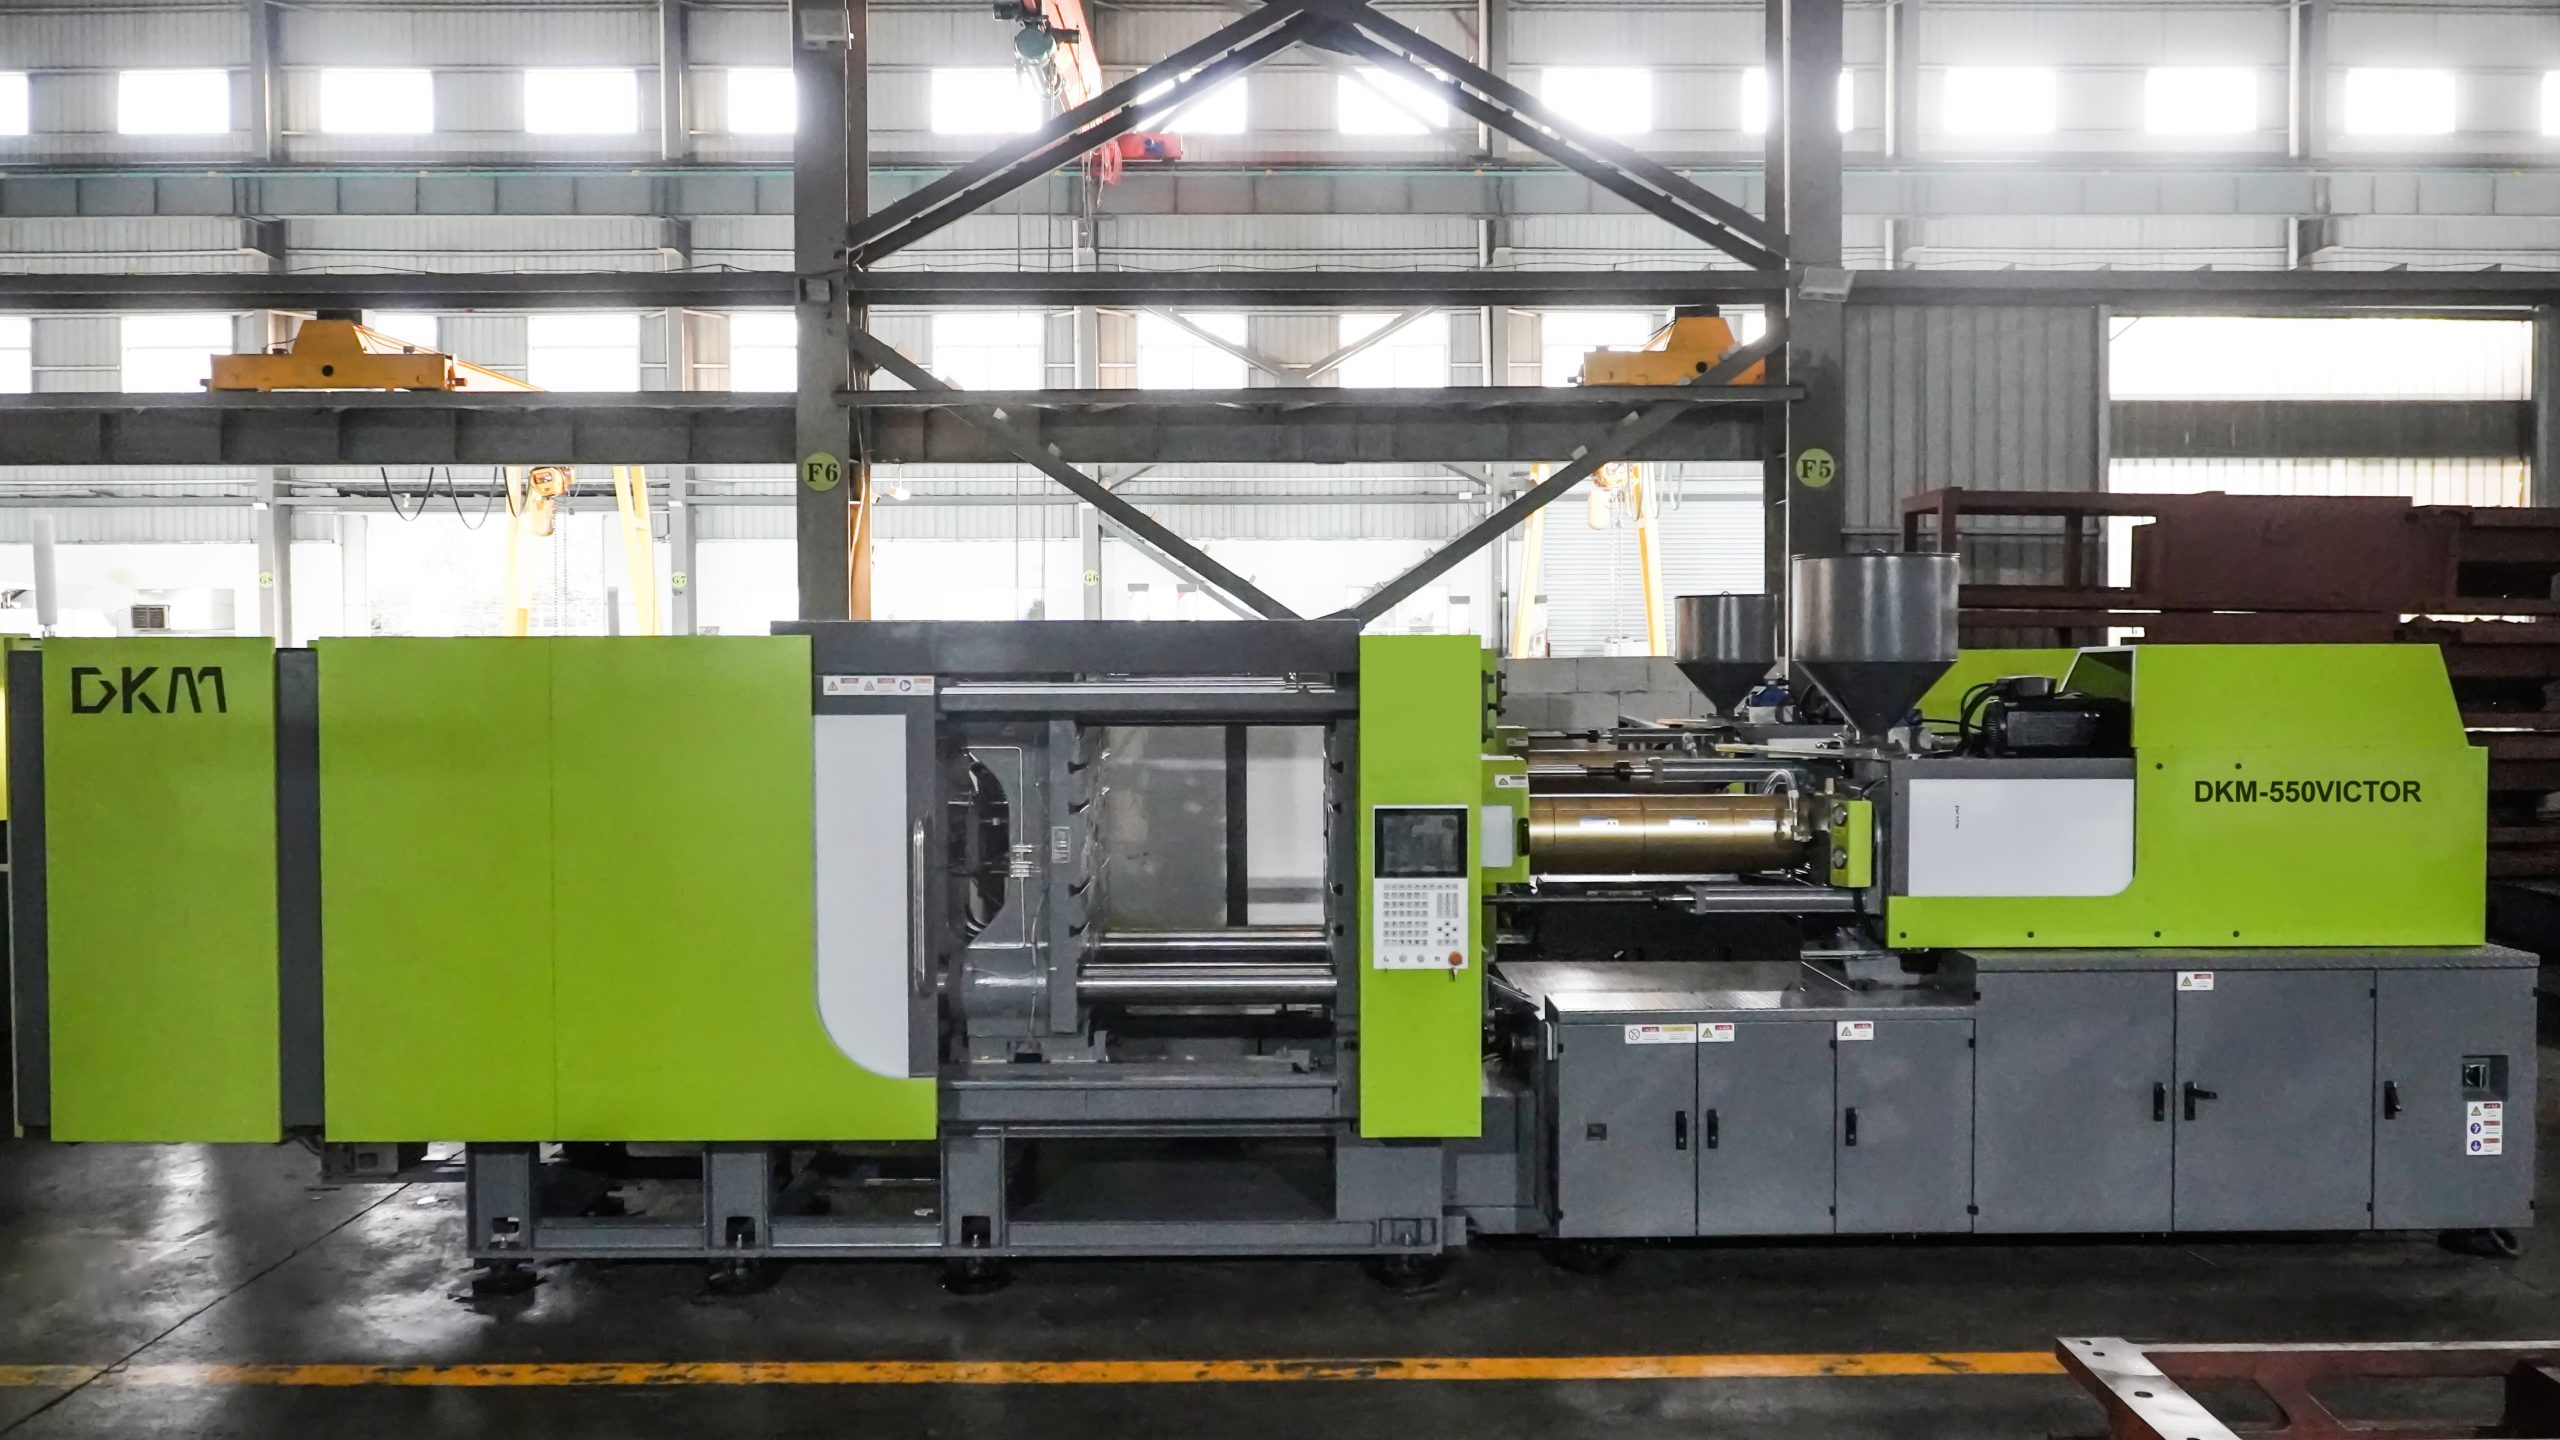
One machine, one mold, and the periphery that protects the cycle. A complete cell pairs a 650–1,000 t fast-speed injection molding machine with a single-cavity hot-runner mold, a 3-axis take-out robot, a cooling conveyor, a beside-the-press granulator, a check scale and packing. Output is set by the slowest link — usually take-out, cooling or packing, not the machine itself.
The format is growing: the plastic pallets, crates and boxes market is forecast to reach USD 37.3 billion by 2033, a 5.8% annual growth rate, according to Grand View Research.
Why one cavity beats two for crates
Clamp force scales with projected area. DKM’s rule of thumb — projected area × 250–300 bar × 1.15 — puts a 600×400 mm crate at 690–830 tf, so 650 t is the floor and 850 t is comfortable. A second cavity doubles the projected area and the mold base (to about 1,600×1,000 mm), needs a 1,300–1,450 t machine and roughly 90% more capital, for about 75% more output.
That trade only pays above roughly 1.2–1.5 million crates a year; below it, single-cavity tooling wins on capex, changeover and maintenance. The same logic carries over to foldable crate lines and pallet box lines, where mechanisms and part size limit multi-cavity tooling anyway.
The machine and the mold
The DKM-650 Victor delivers 6,500 kN of clamp, 900×900 mm tie-bar spacing, 185 mm/s injection speed and a 1,920–3,631 g shot. DKM reports cycles 25–50% shorter than standard machines, with three parallel actions — slide, closing, and mold opening with ejection — that keep non-molding movements out of the cycle.
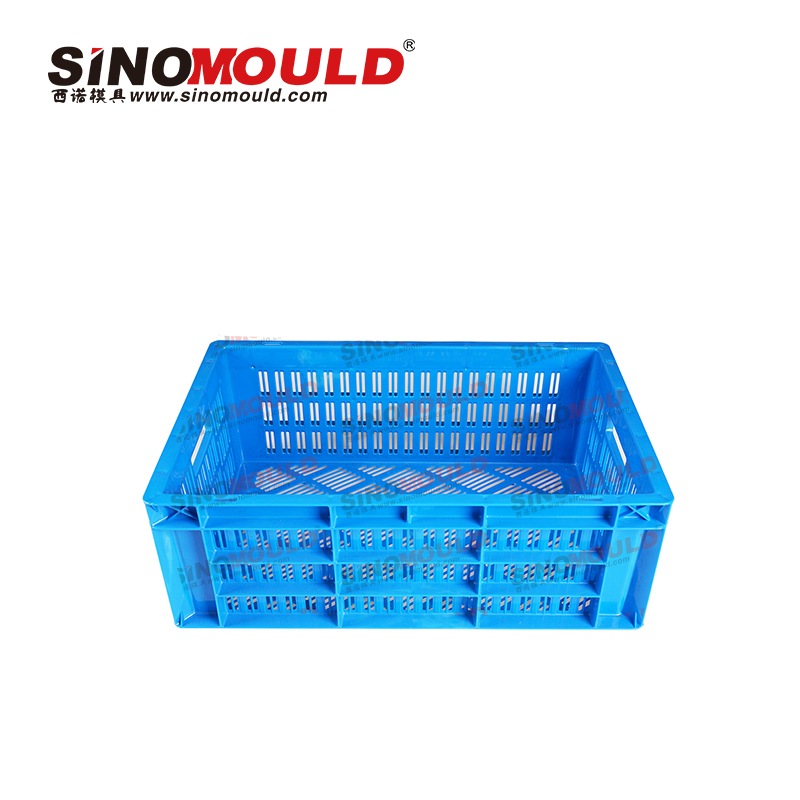
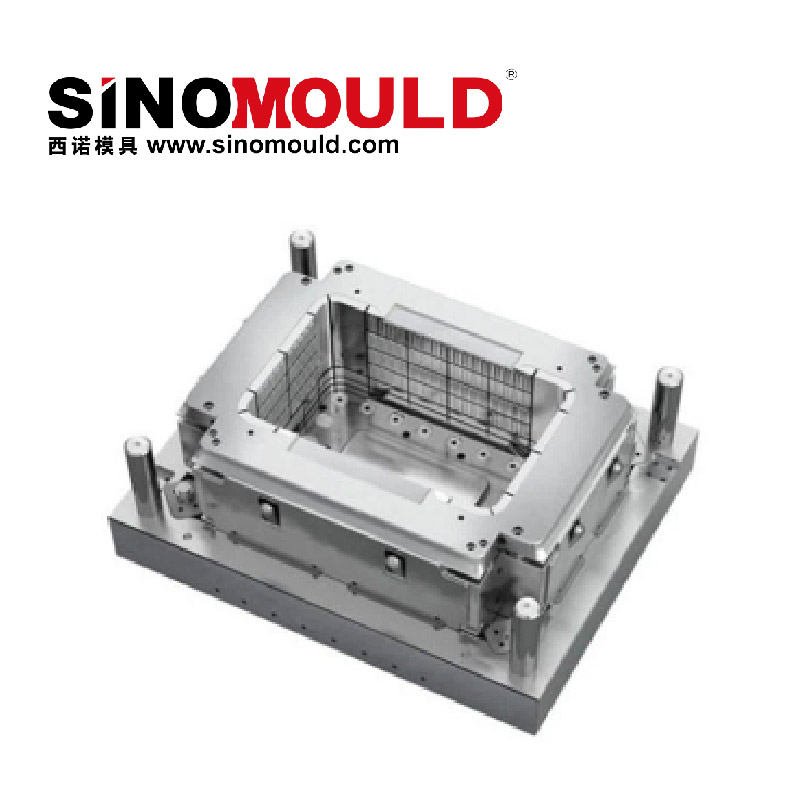
The mold decides the rest. Crate tools use 718H or 738H pre-hardened steel, a valve-gated hot runner and directed core cooling, because cooling takes 60% or more of a crate cycle. SinoMould builds crate tools from 650 to 1,800 t with 15–20 s cycles at 2.5–3.5 mm wall, 800,000–1,000,000 cycles of mold life and about 60 working days of lead time. The reference tool on the one-cavity line molds a 50×30×25 cm turnover box in 20 seconds.
What it produces and what it costs
At 20 seconds, one cavity produces 180 crates an hour gross, 153 at 85% OEE — 3,672 per 24-hour day and about 918,000 a year. Cycle time rises with crate height: DKM’s 2017 field data shows a 600×400×350 mm crate at 35–40 s on a 650 t machine, about 2,100 crates a day.
Unit cost for a 1.6 kg PP crate is about USD 2.75, of which resin is roughly 72%. A 10% resin price move therefore changes crate cost by about 7%, while a 10% machine discount changes it by about 0.2% — which is why buyers should negotiate cycle time, OEE and scrap, not just machine price. A 650 t line with one mold, robot and auxiliaries budgets at roughly USD 210,000–360,000 factory-direct, excluding building and utilities.
Compliance: PPWR and recycled content
The EU Packaging and Packaging Waste Regulation (EU) 2025/40 applies from 12 August 2026. Article 29 requires 40% of listed transport packaging — plastic crates are named — to be reusable by 1 January 2030, and 100% on own-site and same-Member-State routes. Article 7 sets recycled content at 10% by 2030 for food-contact non-PET packaging and 35% for other plastic packaging — not the 30% beverage-bottle figure often quoted for all packaging. Food-contact crates also need an EU 10/2011 declaration of compliance, as on the beverage crate line.
FAQ
One cavity or two? One for most crates: a two-cavity 600×400 tool needs 1,300–1,450 t for about 75% more output at roughly 90% more capital.
How many crates per hour? 180 gross at a 20 s cycle, 153 at 85% OEE — about 918,000 a year.
What tonnage do I need for a 600×400 mm crate? 650 t minimum and 850 t usual for one cavity; 1,300–1,450 t for two cavities.
What does the PPWR require for plastic crates? From 1 January 2030, 40% of listed transport packaging — plastic crates are named — must be reusable within a reuse system, and 100% on own-site and same-Member-State routes. Recycled content starts at 10% by 2030 for food-contact non-PET packaging and 35% for other plastic packaging.
About DKM (Sino Group)
DKM (Zhejiang Dekumar Machinery Co., Ltd.) is a Sino Group brand based in Taizhou, Zhejiang, China. It builds fast-speed injection molding machines from 90 to 4,000 t and turnkey crate lines, with 24+ years in crate production, 1,500+ crate molds and machines, SinoMould tooling, UL 508A-certified machines and 1,600+ customers in 150+ countries. See the one-cavity crate production line and turnkey production solutions.
Related products
-
20KVA/16KW Diesel Generator With Cummins Engine
Contact UsOur 16KW 20KVA diesel generator with Cummins engine is ideal for reliable power solutions.
-
High-efficiency activated carbon attachment device
Contact UsHigh-efficiency activated carbon attachment device can quickly absorb pollutants in exhaust gas. The exhaust gas containing pollutants is powered by a fan and enters the activated carbon adsorber under negative pressure.
-
PP PE LDPE HDPE Film Recycled Plastic Washing Machine Recycling Production Line For Sale
Contact UsThe recycling washing line is mainly used to recycle all kinds of plastics, such as film, agricultural film, greenhouse film, woven bags and etc. it can also recycle waste plastic bottles such as HDPE, LDPE, PP, etc. Our output ranges from 300 kg to 2000 kg per hour. Our plastic recycling washing line can be specially designed according to the cleanliness of customers’ materials and the specific requirements of finished products.
-
Reviews
There are no reviews yet.